Power-Team Hydraulic Tools FAQ: Cylinders, Pump Parts, Rotation Checks, and NF7400X Valves
-
What should I inspect on a Power Team hydraulic cylinder first?
-
How do I verify Power Team hydraulic pump parts are genuine and compatible?
-
How do you check hydraulic pump rotation without damaging the pump?
-
What matters on an NF7400X copper press swing check valve?
-
Is a compound leverage wrench worth it for industrial maintenance?
-
What quality issues do you see most often with hydraulic tools?
-
How do you build an efficient receiving inspection process without slowing everything down?
Quick answer guide: I work as a quality and brand compliance manager for an industrial equipment distributor. I review incoming hydraulic tools before they reach customer job sites—usually 200+ unique SKUs a year. These are the questions I get from maintenance teams, procurement folks, and our own service techs. No long intro, just what I check and why.
- What should I inspect on a Power Team hydraulic cylinder first?
- How do I verify Power Team hydraulic pump parts are genuine and compatible?
- How do you check hydraulic pump rotation without damaging the pump?
- What matters on an NF7400X copper press swing check valve?
- Is a compound leverage wrench worth it for industrial maintenance?
- What quality issues do you see most often with hydraulic tools?
- How do you build an efficient receiving inspection process without slowing everything down?
What should I inspect on a Power Team hydraulic cylinder first?
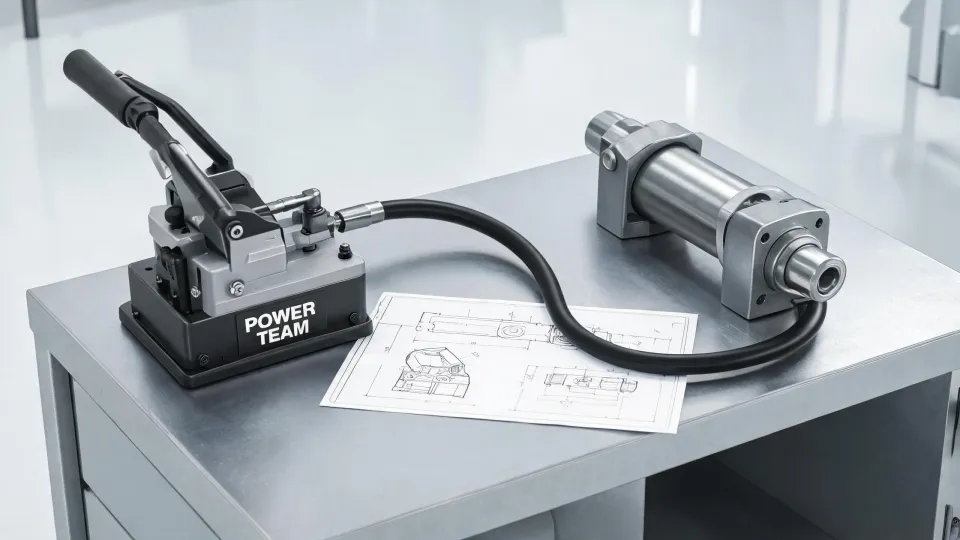
Start with the rod, ports, and stroke label—not the paint. A Power Team hydraulic cylinder can look fine in the crate and still have a scored rod, burred port threads, or a return port that doesn’t match the pump you planned to use. In Q1 2024, we received a batch where the port threads were visibly off—about 0.8 mm against our spec. Normal tolerance was tighter. The vendor claimed it was within industry standard. We rejected the batch, and they redid it at their cost. Now every contract includes port gauge requirements.
Check capacity, collapsed and extended length, mounting pattern, and whether it’s single- or double-acting. Also confirm the serial and label match the paperwork. If it’s going on a press or puller, verify the hose and coupler compatibility before it leaves your dock. That five-minute check is way cheaper than a failed job site.
How do I verify Power Team hydraulic pump parts are genuine and compatible?
Don’t rely on dimensions alone. Power Team hydraulic pump parts can look close and still fail under pressure. I check the part number, serial or batch code, packaging, and supplier authorization. If it’s a critical part—relief valve, manifold, cartridge—I want the spec sheet and a traceable lot number. We didn’t have a formal parts verification process until 2022. Cost us when a lookalike relief valve failed during a 100-ton press test. No injury, but it ruined a seal kit and delayed a customer by three days.
Compatibility is not universal. A pump built for one reservoir, voltage, or control type may not swap into another system. Basically, verify the system schematic, not just the thread size. Plus, use an authorized distributor when downtime matters. The cheaper part is rarely cheaper after a failure.
How do you check hydraulic pump rotation without damaging the pump?
First, read the manual and find the rotation arrow on the pump body. Then confirm the driver rotation before you couple anything. If you can’t see the arrow, use the inlet and outlet layout—but the manual wins. For electric drives, lock out the circuit, bump the motor for 1–2 seconds with the pump uncoupled, and watch the shaft direction. For engine-driven units, check the PTO or belt routing. Never dry-run a pump just to see which way it spins.
I knew I should verify rotation before coupling a replacement pump, but thought, ‘what are the odds?’ The odds caught up with me when it ran backward and scored the shaft in under 30 seconds. That was a $1,800 mistake and a lesson I still repeat to new techs. Use a pressure gauge and flow check after start-up, and confirm temperature and noise are normal.
Per ISO 4413:2010, hydraulic systems and components must be selected, applied, and maintained according to the manufacturer’s specifications. For U.S. service work, OSHA 29 CFR 1910.147 sets the lockout/tagout baseline before you touch the drive.
What matters on an NF7400X copper press swing check valve?
For an NF7400X copper press swing check valve, the details matter more than the box label. Check the press connection size and compatibility with your copper tube, the pressure and temperature rating, seal material, and flow direction arrow. A swing check valve is not a commodity item—install it backward or with the wrong seal, and it can leak on the first pressure test. In my opinion, the spec sheet should be reviewed by the same person who signs off on the press tool jaws.
We had a batch where the arrow was stamped opposite the internal flow path. That would have been a callback on a commercial job. Now we verify flow direction with a flashlight and a low-pressure air test before stocking. Also confirm the valve is rated for the system fluid and that the press connection meets the project specification. If you’re mixing brands, don’t assume the jaws or fittings are interchangeable without checking.
Is a compound leverage wrench worth it for industrial maintenance?
Usually, yes—for repetitive work in tight spaces. A compound leverage wrench multiplies force, so you get more torque with less operator fatigue. It’s not a replacement for a hydraulic torque wrench on high-spec flanges, but it can be a smart step between a standard breaker bar and a full hydraulic setup. Check the torque multiplication, reaction arm, handle length, and calibration requirements. Also confirm it fits the fasteners you actually have, not just the catalog photo.
I ran a blind test with our team: same tech, same flange, compound leverage wrench vs. a standard breaker bar. Seven out of ten identified the compound tool as ‘more controlled’ without knowing the difference. The cost increase was about $40 per tool. On a 120-tool kit, that’s $4,800 for measurably better feel and less fatigue. From my perspective, that’s worth it if your techs do a ton of manual bolting.
What quality issues do you see most often with hydraulic tools?
Contamination, wrong fluid, damaged threads, counterfeit parts, missing labels, and bad storage. These rarely show up as a dramatic failure at first. They show up as a slow pressure drop, a sticking valve, or a cylinder that won’t retract. Most are preventable with proper specs and inbound checks. We didn’t have a formal inbound inspection process until 2022. That cost us when a cylinder with a scored rod went to a customer. The defect ruined the job and we ate the return freight.
The third time we ordered the wrong seal kit, I finally created a verification checklist. Should have done it after the first time. Now we photograph every serial number and compare it to the purchase order. It takes maybe 90 seconds per item, but it has cut our wrong-part rate by more than half. The goal isn’t perfect paperwork; it’s fewer surprises on site.
How do you build an efficient receiving inspection process without slowing everything down?
Use risk-based inspection, not one-size-fits-all. High-mix custom items get 100% inspection. Standard catalog items get sampling based on supplier history. We switched to digital checklists and QR labels in 2023. That cut our turnaround from 5 days to 2 days. The automated process eliminated the data entry errors we used to have, and it made supplier scorecards actually useful.
Start with three fields: part number, serial or lot, and inspection result. Add photos only for exceptions. Then review the data monthly. If a supplier has three clean lots, reduce sampling. If they have one bad lot, increase it. That’s efficiency without pretending every item deserves the same scrutiny. Traditional paper checklists still work for small shops, but for us, the digital step was the difference between checking boxes and actually catching problems.
Rajiv Menon
Rajiv Menon is an independent rigging and lifting hardware analyst covering shackles, chain hoists, hooks, turnbuckles, wire-rope clips, and lifting attachments. He applies ISO 2415:2022 shackle requirements while evaluating working load limit, grade, proof load, design factor, pin fit, sling angle, reeving, brake behavior, identification, inspection, and temperature range. His safety-led guides help lifting teams and purchasers select compatible hardware, interpret markings, establish inspection criteria, and avoid side loading or undocumented substitutions.